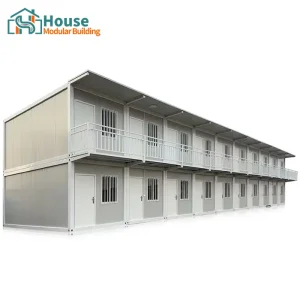
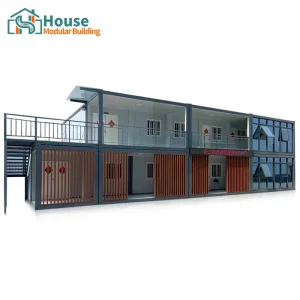
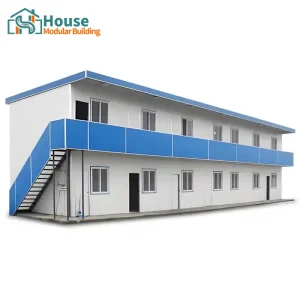
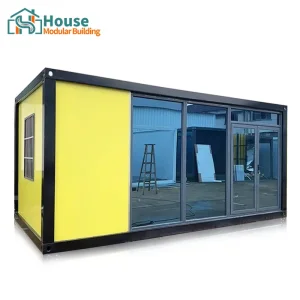
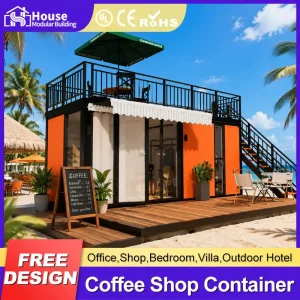
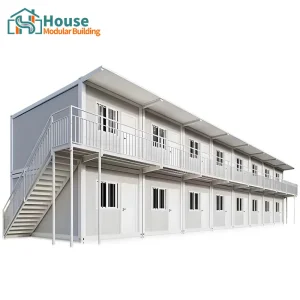
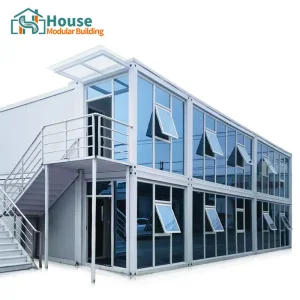
Explore our premium range of factory-certified prefabricated modules designed for heavy structural deployment and high thermal rating compliance.
Expert Technicians
R&D Engineers
Avg. Core Experience
BCA / NCC Compliant
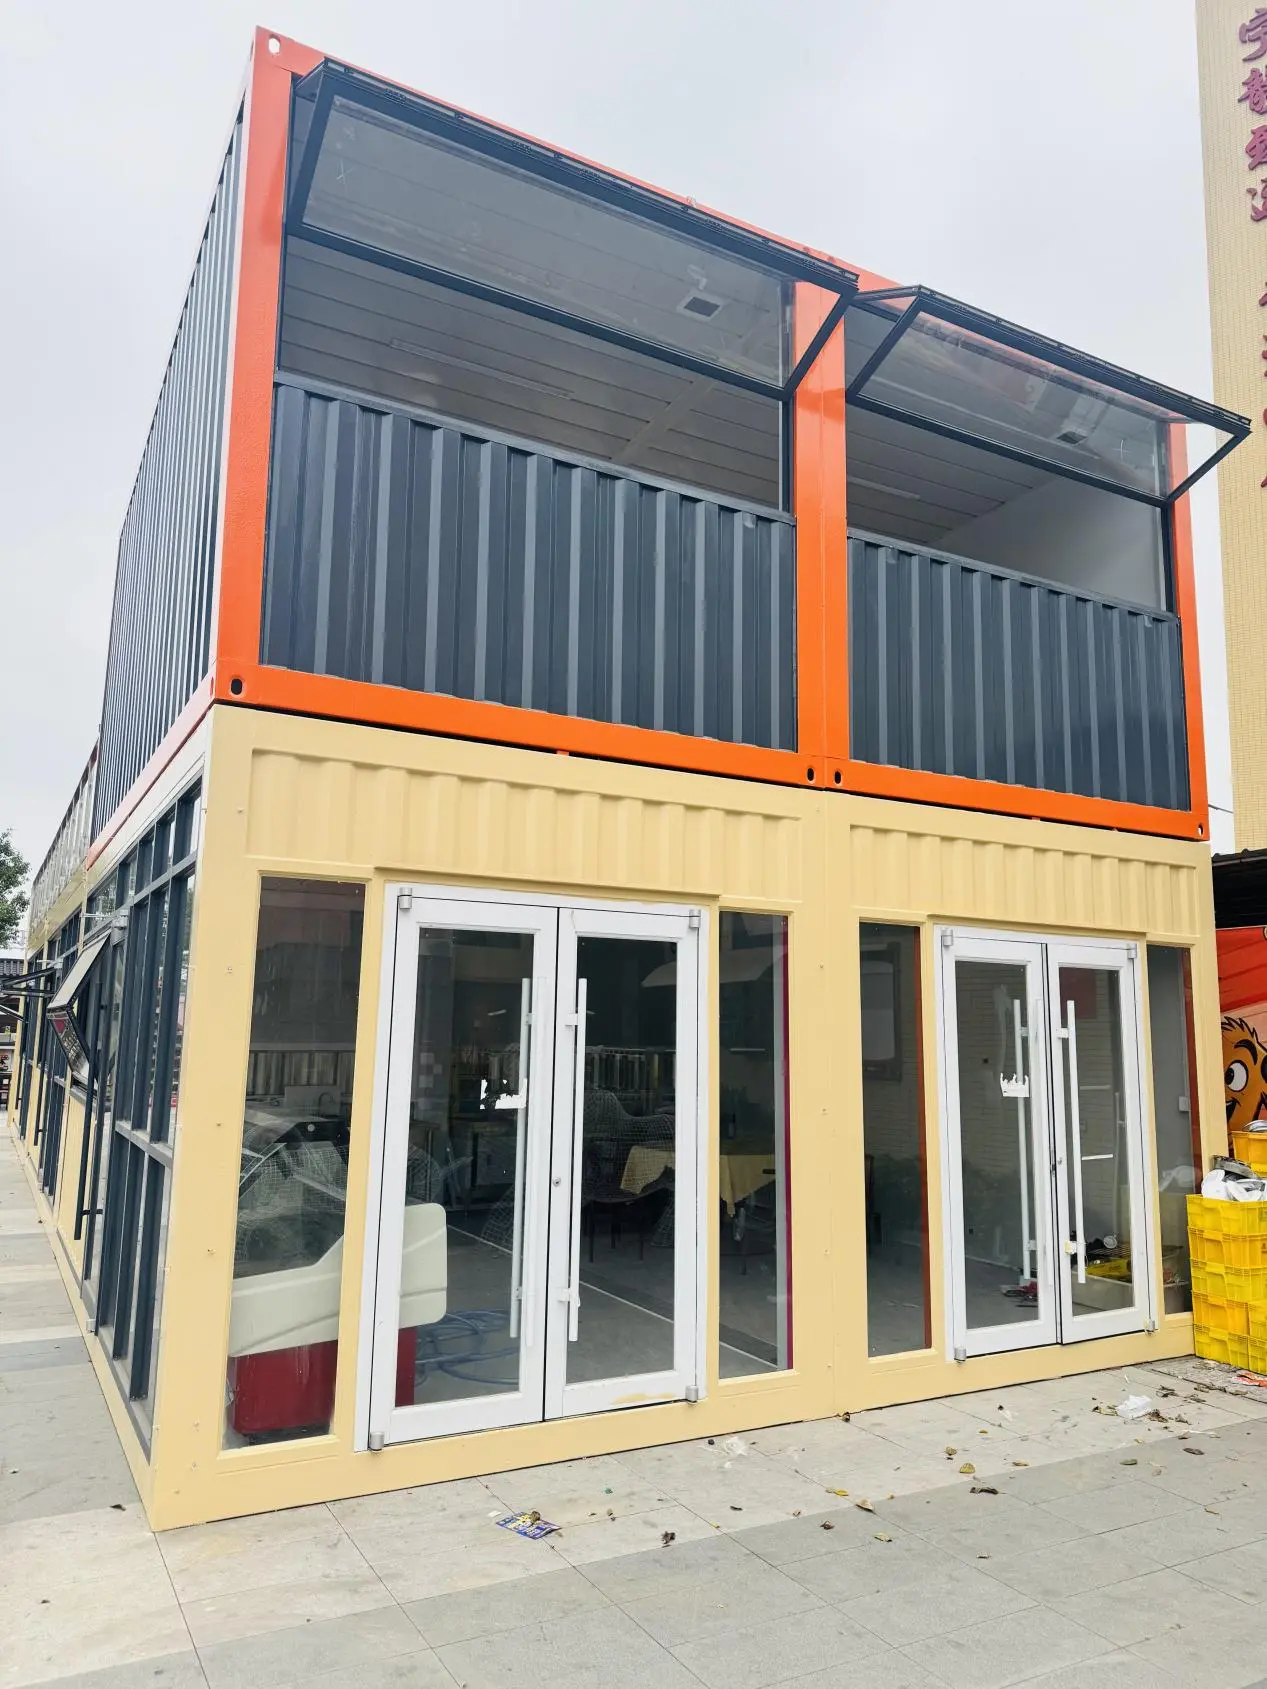
The contemporary Australian housing landscape is shaped by rising construction costs, prolonged build cycles, and severe climate realities. Architects and owners inspired by high-end modernism are increasingly utilizing modular container homes to achieve clear architectural expressions within accelerated timelines. However, creating a bespoke container home that meets the standards of high-end structural design requires far more than merely positioning retired ISO shipping containers. It requires precision-manufactured, customized structural modules that balance structural integrity with aesthetic elegance.
From cantilevered multi-level pavilions in the Dandenong Ranges to minimalist linear eco-cabins overlooking the rugged coastline of South Australia, the aesthetic is defined by expansive glazing, open-plan structural spans, and seamless integration with the surrounding topography. Our OEM services enable design practices to specify custom dimensions, integrated structural steel beams (columns and cross-members), and continuous thermal breaks that mitigate the limitations of traditional container conversions.
To successfully deploy modular housing across Australia's distinct geographical zones, specific engineering modifications are integrated directly at the factory level:
For installations in bushfire-prone zones (such as rural Victoria or New South Wales), structures are engineered to meet BAL-29, BAL-40, or BAL-FZ (Flame Zone) criteria. This includes non-combustible exterior cladding (fiber cement or steel alloy), fire-rated rockwool wall insulation, and double-glazed toughened safety glass with aluminum framing.
For coastal Western Australia and Northern Queensland, our container bases are engineered with reinforced corner castings, heavier wall profiles, and specialized anchor tie-down brackets. They are rated up to wind class C3/C4 and tested under severe cyclic loading simulations.
Deployments in the Snowy Mountains or Tasmania feature continuous exterior thermal barriers to eliminate thermal bridging through the steel columns. Integrated subfloor heating and high-density polyurethane insulation maintain internal climate stability with minimal energy draw.
Self-contained living blocks equipped with plug-and-play solar array mounts, greywater treatment loops, and high-capacity battery compartments, designed for immediate placement and hookup in remote locations.
Our engineering roadmap prioritizes sustainability, structural longevity, and energy efficiency. Below is an overview of the materials and systems built into our OEM line:
A breakdown of the engineering steps we take to ensure our modular homes last a lifetime in harsh coastal, alpine, or arid regions.
All load-bearing nodes are welded using automated robotic arms to ensure depth, consistency, and structural load distribution that exceeds manual standards.
Electrical and plumbing conduits are pre-machined and installed within the wall cavities using fire-retardant sleeves, conforming to AS/NZS 3000 standards.
Designed for severe marine environments, our frames undergo abrasive blasting before receiving a multi-layer epoxy primer and polyurethane topcoat paint system.
The primary advantage of collaborating with a Chinese OEM manufacturer like House Modular Building lies in our deeply integrated supply chain. Producing high-performance modular units at a competitive price point requires access to raw steel mill materials, automated manufacturing lines, and specialized hardware suppliers within close proximity.
With dedicated manufacturing bases in both the North and South of China, we provide specialized logistical and logistical flexibility. The northern facility focuses on high-capacity steel processing and heavy structural fabrication, while our southern plant specializes in custom finishes, electrical assembly, and international logistics operations. This dual-base strategy ensures that production schedules remain uninterrupted, regardless of regional environmental factors or transport constraints.
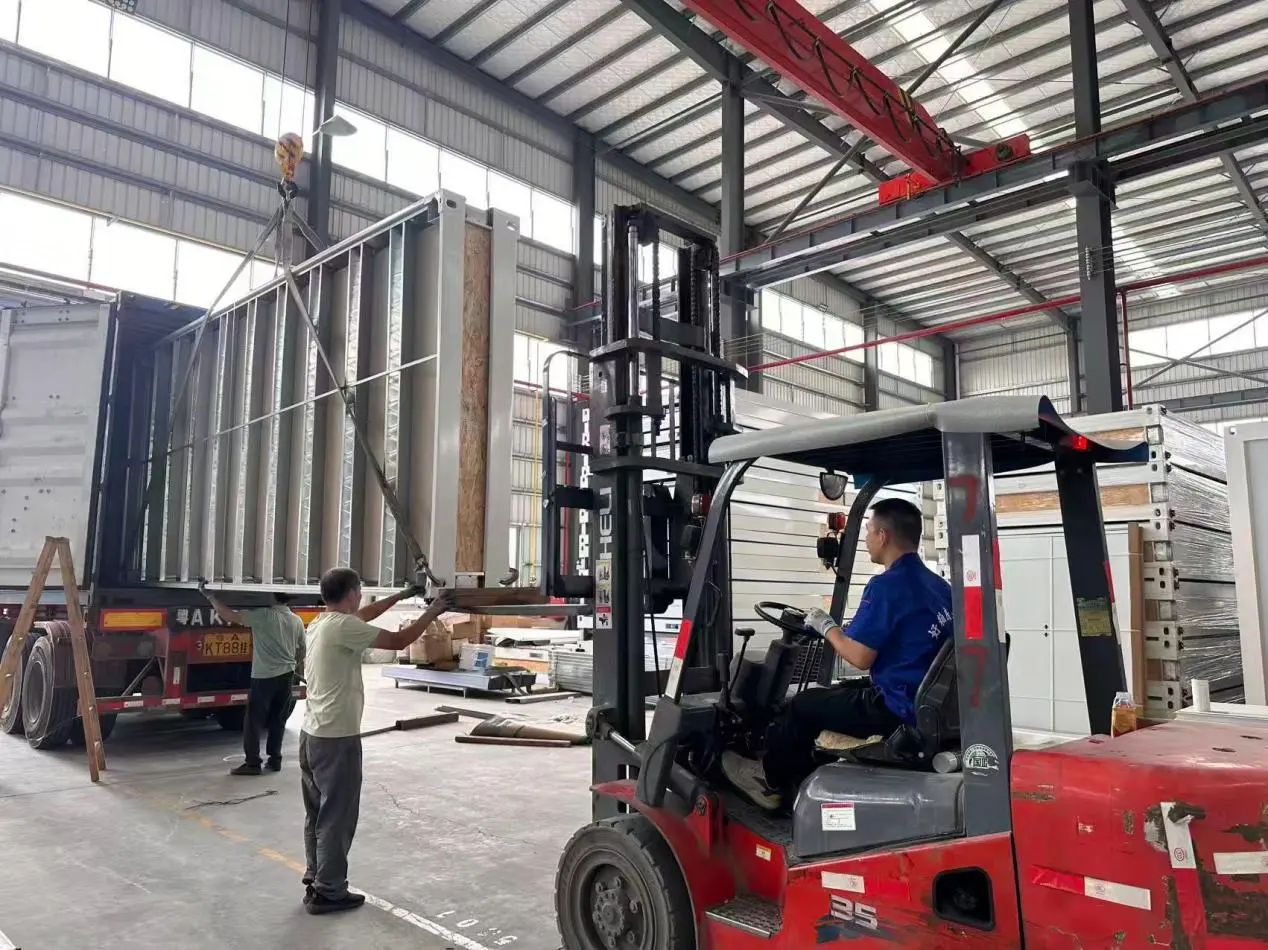
Every piece of structural steel used in our facility is trace-certified from reputable domestic mills. Our internal quality assurance protocols require non-destructive testing (NDT) of critical structural welds, load-bearing deflection analysis, and hydrostatic testing of all pre-plumbed wet areas prior to packing and container loading.
By standardizing component dimensions and utilizing advanced ERP manufacturing tracking systems, we minimize material waste to less than 2%, passing these cost savings directly to our international distribution partners.
A trusted manufacturing partner delivering high-quality modular houses and pre-engineered residential frames worldwide.
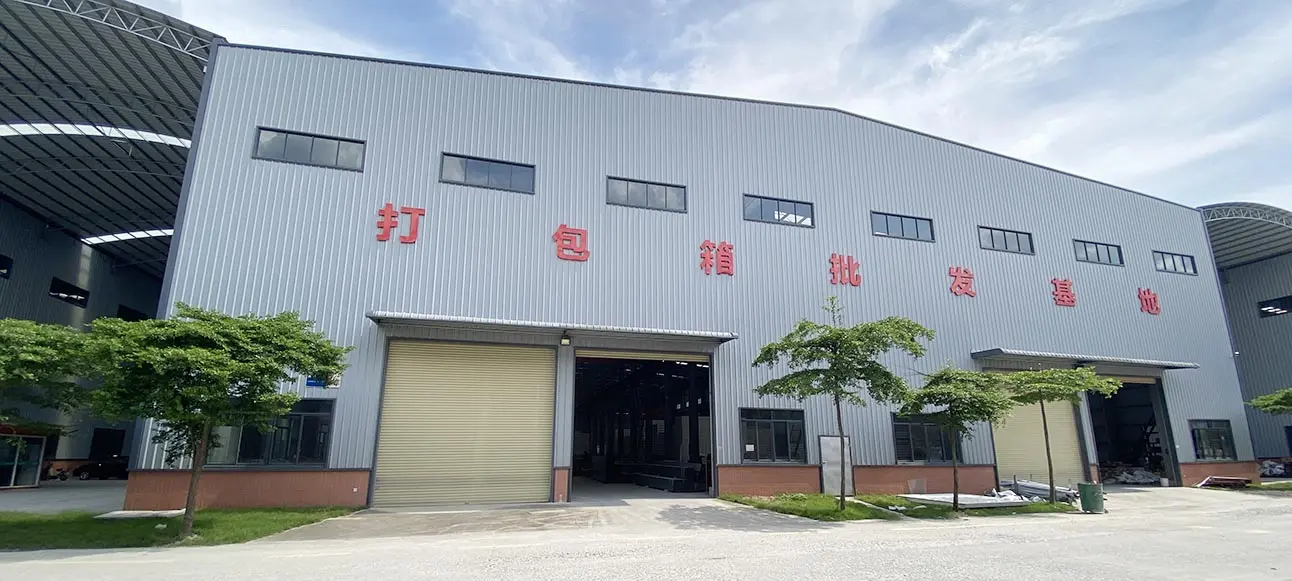
House Modular Building has rich professional knowledge and experience in the production of container houses and prefabricated houses. The company features a dedicated architectural design team to provide solution designs tailored to each customer's specific project needs, and a technical sales team to manage order tracking and logistical coordination. Our factories ensure prompt product delivery while maintaining high quality standards and production efficiency.
In order to better serve customers and demonstrate our production and delivery capabilities, we have established production bases in both the North and South of China to provide efficient delivery solutions for diverse national standards. We support OEM and ODM operations in our factory for different countries, and provide distributors with a mutually beneficial partnership.
With consistent customer satisfaction, our team has built comprehensive service capabilities and business technology coverage. This spans from raw material processing to foundation construction planning and the implementation of complete service systems.
House Modular is a production-oriented enterprise. The factory has a senior professional, independent research and development team, and currently employs more than 200 staff. Among them, technical personnel such as structure and frame R&D account for more than 30% of the total workforce. More than 60% of our employees have over 5 years of experience in the modular fabrication industry, and core team members have worked in the building materials field for more than 10 years. As a professional supplier of container houses, we maintain a strong team to support customers and solve their custom design challenges.
Importing prefabricated structures into highly regulated markets like Australia, New Zealand, the United States, and Western Europe requires strict adherence to local building standards. House Modular Building addresses these requirements during the initial engineering design phase:
Get answers to common technical, logistics, compliance, and customization questions regarding our container homes.
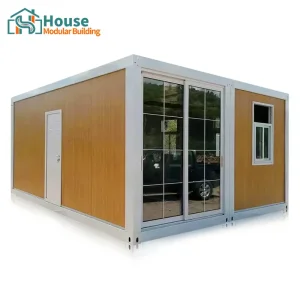
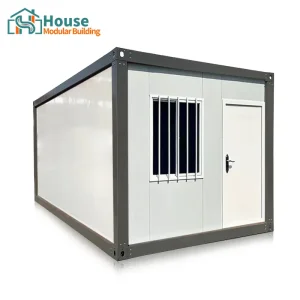
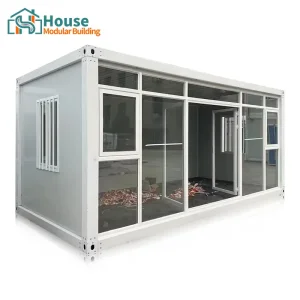
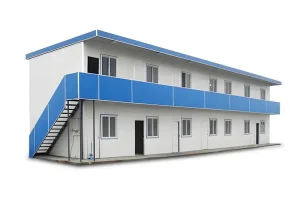
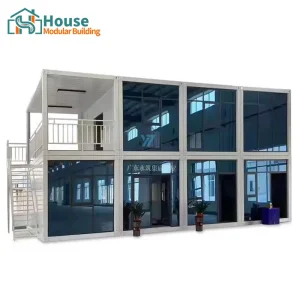
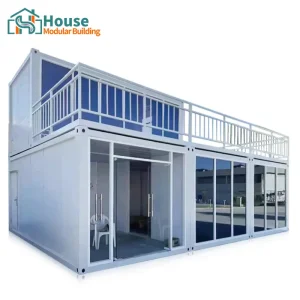
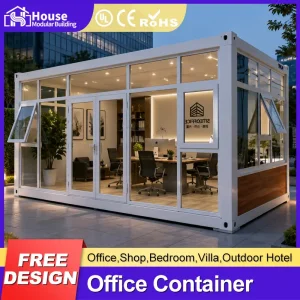
Discover our range of modular solutions, including heavy-duty workspaces, site accommodations, and commercial glass facade units.
 House Modular Building