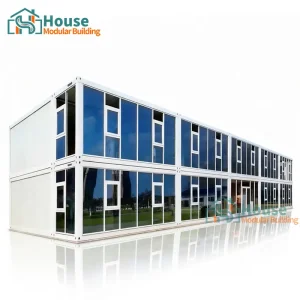
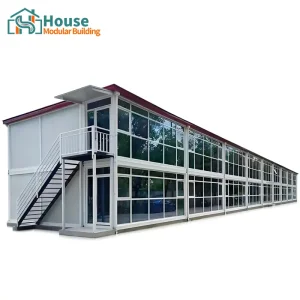
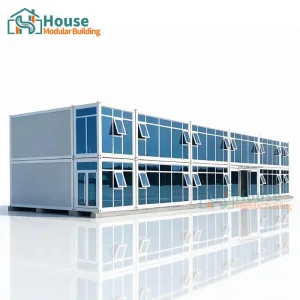
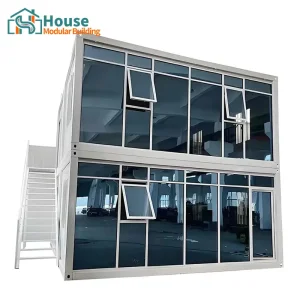
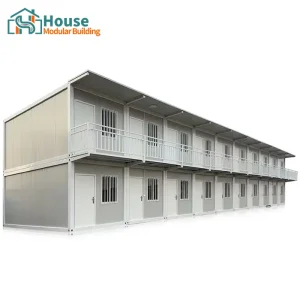
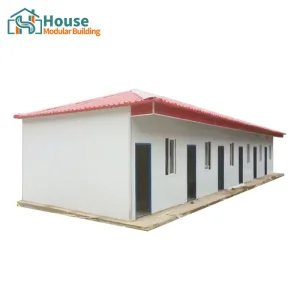
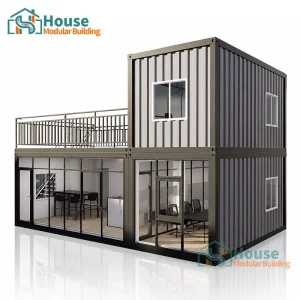
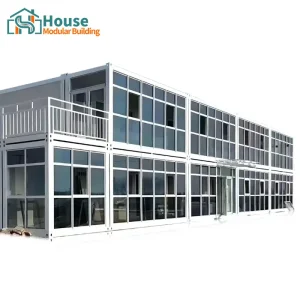
Industrial grade customized units designed for commercial applications, remote workforces, and executive environments.
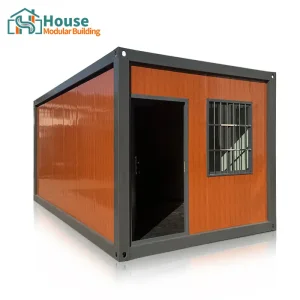
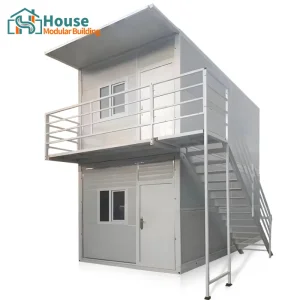
The modern construction landscape is undergoing a paradigm shift towards industrialized, off-site construction methods. Modular container buildings, once utilized predominantly for temporary storage, have evolved into a core solution for high-density housing, commercial complexes, and rapid industrial deployment globally.
By transforming raw structural steel and high-efficiency insulation panels into standardized, intermodal volumetric units, global developers are mitigating traditional construction pain points: rising labor costs, unpredictable weather, and extended project timelines. Our modular structures conform to strict international building codes (IBC), structural standards (EN 1090), and localized thermal performance requirements, ensuring that each structural unit functions as a permanent or semi-permanent asset.
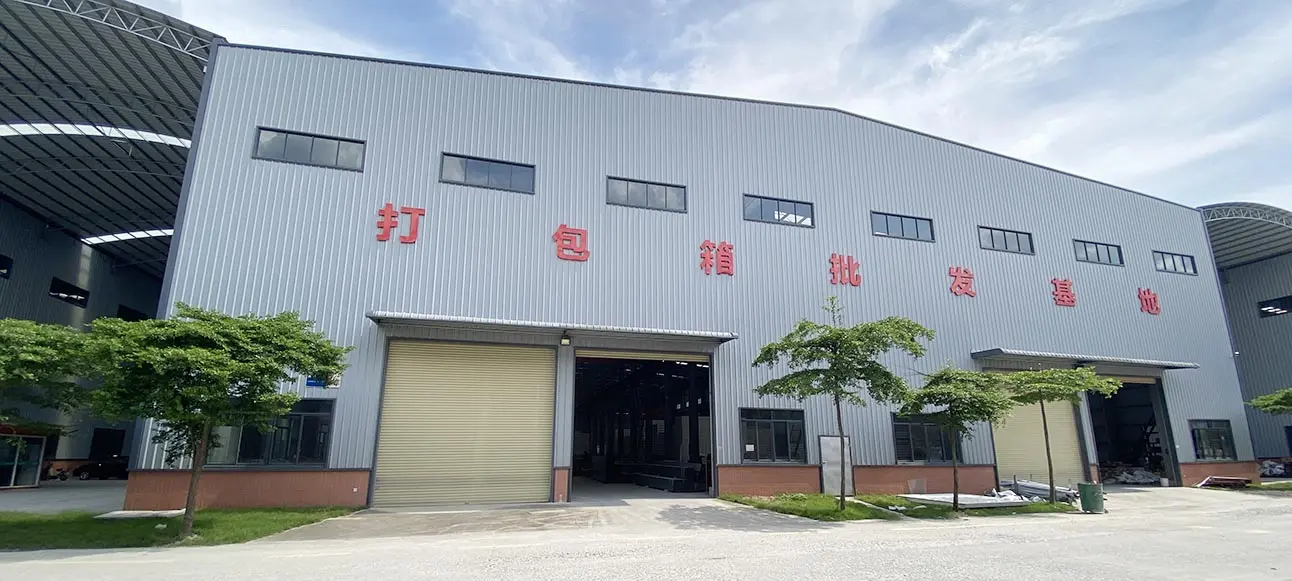
Strategic geographic footprint and vertical supply chain integration driving cost efficiency and speed.

To optimize shipping routes and minimize global freight costs, House Modular Building has established extensive production bases in both the North and South of China. This strategic layout enables us to facilitate rapid maritime export via key ports, matching local distributor demands across the Americas, Europe, the Middle East, and the Asia-Pacific region.
Our operation model is fully optimized for OEM and ODM requirements. By keeping core material manufacturing in-house, we exercise granular control over every aspect of structural assembly. Our manufacturing floor processes use high-strength Q355B structural steel, continuous automatic welding lines, and advanced anti-corrosion coating procedures, offering highly competitive wholesale prices without compromising structural integrity.
As a leading supplier of modular container buildings, House Modular combines a robust design capability with deep industrial knowledge. Our technical R&D division represents over 30% of our workforce, ensuring we stay at the forefront of structural engineering, building envelope physics, and insulation technologies.
We work from the raw material level upward, managing structural steel framing configurations, internal wall layouts, and customized aesthetic cladding options (such as modern glass curtain walls or structural insulated paneling systems). Our specialized engineering team handles:
How our OEM container solutions are deployed across diverse sectors and environmental conditions.
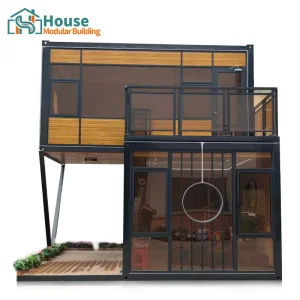
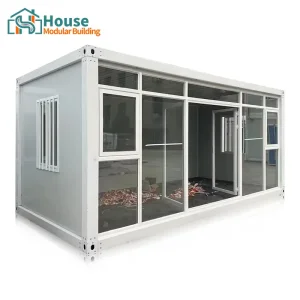
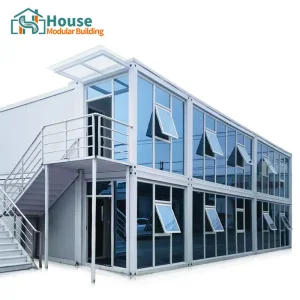
From single-unit administration offices on job sites to large-scale double-story luxury office buildings. These setups feature glass facades, integrated lounges, and structural modifications to support high-occupancy workspaces.
Designed for resource sectors such as mining, oil, gas, and major infrastructure installations. Our modular worker dormitories offer high structural strength, optimized HVAC integration, and easy sanitary hookups.
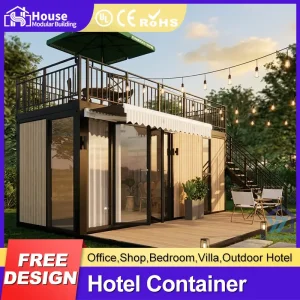
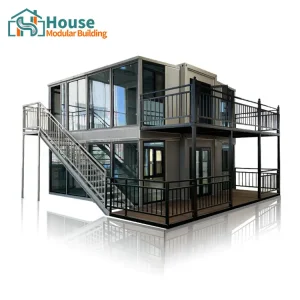
High-end modular container houses and modular hotels designed with modern aesthetics. Features include rooftop terraces, folding balconies, double-glazed windows, and premium internal finishes for direct tourist rental.
Maximizing project value through standardized sizing, efficient packaging, and optimized shipping logistics.
We work directly with your architectural drafts. Our 3D BIM modeling team produces engineering plans mapping structural loads, thermal performance levels, and interior custom features prior to manufacturing.
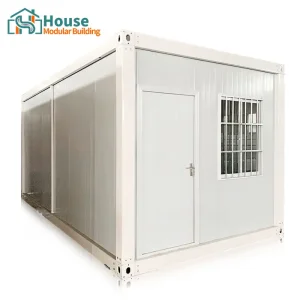
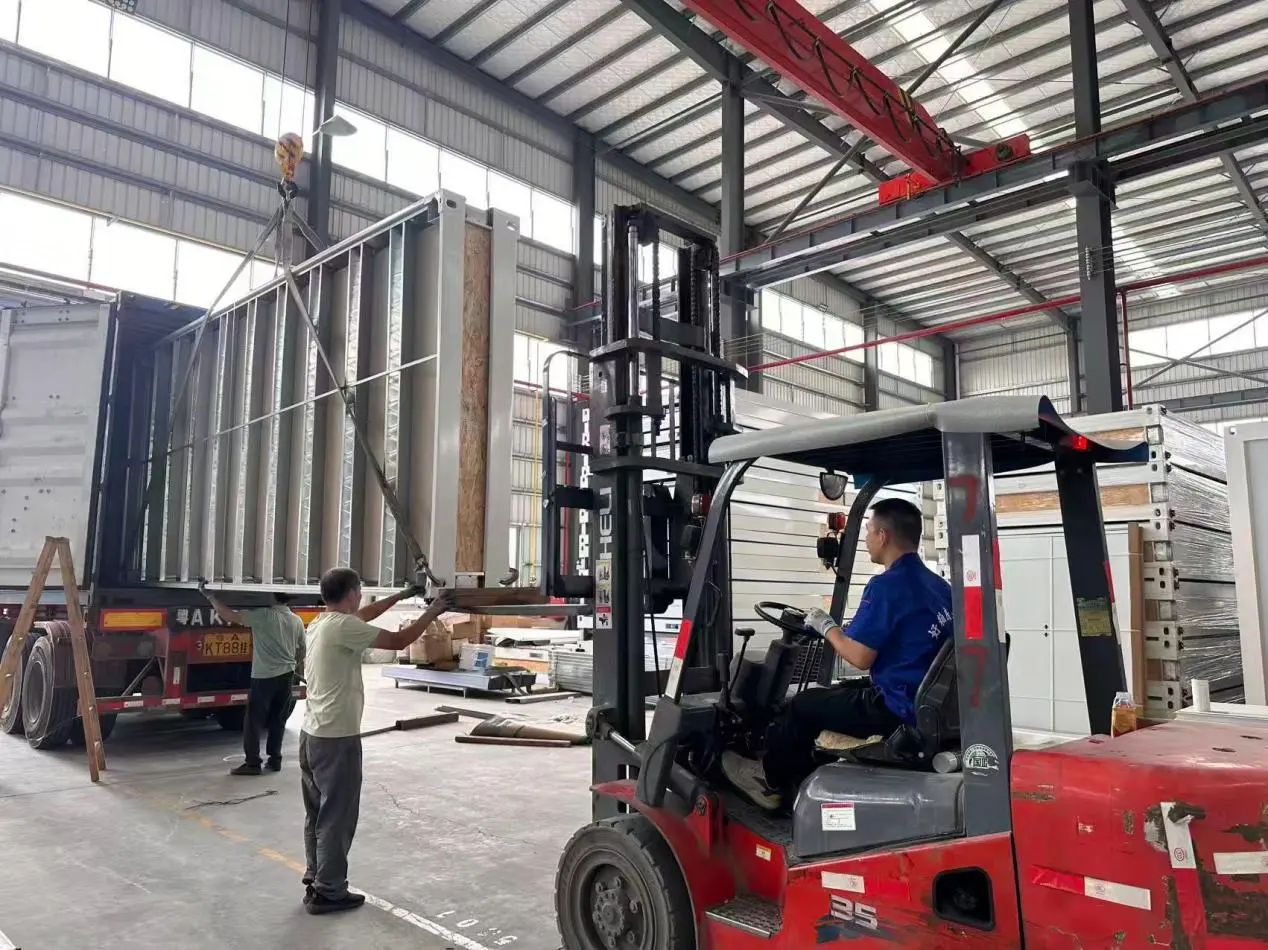
To reduce freight overhead, we offer flat-pack configurations where up to 4 flat-pack units are bundled as a single standard 20ft shipping container dimensions. This saves up to 75% on maritime freight costs compared to rigid structural units.
Our quick-assembly units are designed for rapid field assembly. Standard tools and a mobile crane are all that are required to assemble and seal a standard 20ft modular cabin within hours, minimizing on-site labor costs.
The global construction industry is shifting toward zero-carbon manufacturing and high circularity. The modular buildings market is moving fast in these directions:
Global procurement teams often struggle with inconsistent manufacturing tolerances, localized regulatory bottlenecks, and shipping delays. House Modular solves these operational pain points through rigorous QA/QC inspection protocols, third-party structural certifications, and comprehensive cargo tracking from our northern and southern Chinese ports.
By partnering with local distributors, we establish reliable supply channels, supplying standardized container modules that easily pass local inspections and building permitting processes in destination markets.
Essential technical and structural guidelines for international procurement managers.
We manufacture our primary structural frames using high-grade Q235B or Q355B structural carbon steel. Frame components undergo hot-dip galvanization (minimum 275g/㎡ zinc coating thickness) followed by an industrial-grade epoxy primer and polyurethane finishing coats to prevent rust in harsh coastal or tropical environments.
We utilize flat-pack and knock-down shipping configurations. For standard 20ft quick-assembly container cabins, four individual flat-packed modules pack down together to match the exact size and corners of a standard ISO 20ft shipping container, meaning they can ship as a single SOC (Shipper Owned Container) or inside standard 40ft high cube dry vans.
Yes. For high-latitude installations, we upgrade structural roof configurations to handle snow loads exceeding 1.5 kN/㎡. Additionally, we replace standard EPS insulation with high-performance PU (polyurethane) or continuous structural mineral wool panels, providing low thermal transmittance values (U-values) that meet North American and European energy codes.
Yes, we customize electrical wiring, conduit configurations, outlets, breaker boxes, and plumbing fixtures to match destination market codes: UL/CSA (North America), CE/EN (Europe), and SAA/WaterMark (Australia and New Zealand). All internal fixtures are tested at the factory before packing.
With standard foundation planning, proper joint sealing, and basic external maintenance, our modular container structures have a structural design life of 15 to 20 years for temporary or semi-permanent placements, and even longer when sheltered or incorporated into permanent foundation designs.
Additional modular configurations including dual-unit configurations, two-story structures, and temporary offices.
 House Modular Building